Home / Services / Electrical / Control Cabinet
Electrical · Miami, FL
Control Cabinet Ice Blasting
When people call about control cabinet, the constraint is usually the same. We clean it without water, without chemicals and without anything abrasive touching the surface.
What builds up, and why it matters
On this kind of work the problem is conductive dust, carbon tracking, oil mist and contamination on insulators and bus. This is the work that makes the low-moisture part of the process matter. You cannot wash a panel. You cannot blast grit into a motor. Dry ice leaves no standing water in a harness, a winding or a cabinet.
Equipment is de-energized and the area ventilated before anything starts. The people who call us about control cabinet are usually facility electricians and reliability engineers, and the thing they are actually worried about is a flashover, or moisture left where moisture should never be.
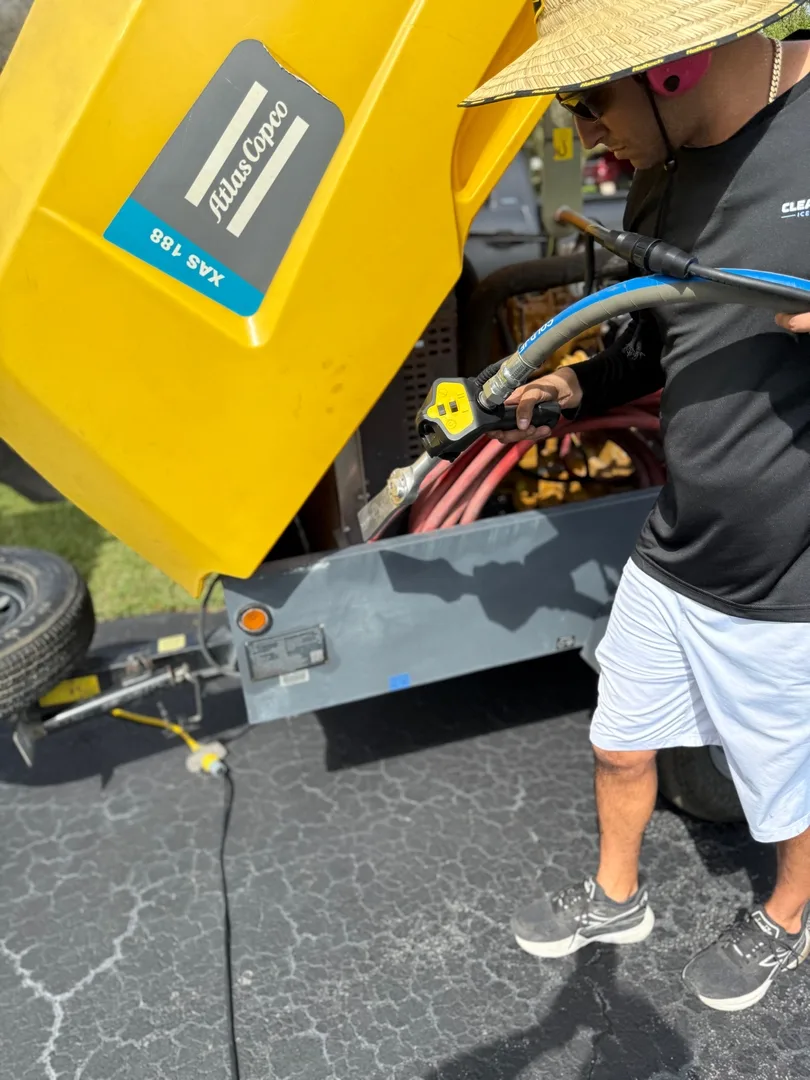
The method
Why dry ice and not the alternatives
- Non-abrasive
The pellet is soft and sublimates on impact, so the work is thermal rather than mechanical. Machined faces, plating, paint and gaskets survive it.
- Low moisture
No standing water in a harness, a bearing or a cabinet, and no dry time before the equipment goes back into service.
- No secondary waste
Sand, soda and walnut shell all have to be swept and hauled. Dry ice leaves only the contaminant it removed.
- Often no teardown
Much of this work is done in place, which is usually where the real saving is. The labor is in the disassembly, not the cleaning.
More electrical work
Related jobs we get called for
Questions we get asked first
Will it damage the surface underneath?
On most substrates, no. The pellet is soft and sublimates on impact, so it does thermal work rather than mechanical work. We still test an inconspicuous spot first on anything unusual.
Do you have to take the equipment apart for control cabinet?
Usually far less than you would expect, and often not at all. Cleaning in place is where most of the saving comes from, because the labor is normally in the teardown and reassembly.
How much mess does it make?
Far less than the alternatives, because the blasting media disappears. What is left is the contaminant itself, which we contain and clean up.
Do you come to us?
Yes. The whole rig is mobile. Compressor, hose and operator arrive at your shop, plant, driveway or dock, anywhere across South Florida from Miami out to roughly a hundred miles.
What does a job cost?
It depends on the equipment, the contaminant and the access, so we will not throw a number at you over the phone without understanding the work. Describe the job and we will give you a real figure.
How soon can you look at it?
Send photos and a short description and one of the owners gets back to you. If you have a shutdown or a deadline, say so up front and we will tell you honestly whether we can hit it.
The comparison
How this compares to the usual methods
- Solvent and degreaser
Softens the contaminant but leaves a film, fumes and a disposal problem, and attacks finishes you meant to keep.
- Hand scraping
Slow enough to be uneconomic on a machine, and the tool always leaves a trace.
- Media blasting
Cuts into the substrate by design. Fine on structural steel, wrong on aluminum, plating, machined faces or anything with a tolerance.
- Pressure washing
It is fast and it is wet, which is fine outdoors and unusable on anything with a winding in it.
- Dry ice
The deposit shrinks away from the surface it is stuck to and releases. The ice is gone before it can do any harm.
What comes off
What this takes off
The method does not care much what the contaminant is, only that it sits on top of something. Here is the usual list.
- Ink and printing residue
Ink and coating on anilox and press rollers, surfaces where changing the texture changes the print.
- Food residue
Carbonized product build-up in a plant where neither standing water nor a chemical film is acceptable.
- Grease and oil
The greasy base coat that traps grit and dust. It releases early and takes the loose material with it.
- Carbon and soot
Baked carbon on a manifold, oven or weld fixture. Thermal shock is exactly the wrong thing for the bond holding it on, which is why this works.
- Adhesive and sealant
The stubborn film under old tape, or the gasket that tore and left half of itself behind.
- Resin and mold release
Cured process residue on a mold or fixture. The surface has to come out dimensionally unchanged, which rules out anything abrasive.
- Paint and coatings
Taken off in a controlled way when what is underneath matters more than speed.
How a job runs
The sequence, start to finish
There is no mystery to how these jobs run, and no part of it we would rather you did not ask about.
- We look at access and containment
Hose run, compressor position, what needs masking, and where the contaminant is collected. For food and electrical jobs the containment plan takes longer to settle than the blasting does.
- We test a small area
Pressure and pellet size get dialed in on an inconspicuous spot before we touch anything visible. Painted parts, soft alloys and older finishes all behave differently, and the right setting on one is the wrong setting on another.
- We blast, then clean up
Nothing is left of the pellet, so the only thing to collect is what was on your equipment. That collection is part of the work we quoted.
- You look before we pack up
A second pass while everything is still connected is free in every sense. A return trip is not.
- You describe the job
Send images if you can, they settle most of the questions. A wrong-tool verdict comes on that first call, not after the invoice.
Before we turn the rig on
This is not a quiet method. Ear defenders are standard issue on site for anyone nearby.
Surfaces come out cold. On some jobs that means waiting a few minutes before handling, and on others it means condensation as the part returns to ambient temperature.
Air comes from our own compressor. You do not need to provide power, water or a connection of any kind.
Anything nearby that should not be touched gets masked before we start. That is quicker than explaining it afterward.
Tell us what needs cleaning.
Give us the job, the address and a rough description, pictures if you have them. The call back comes from Giancarlo or Kenny directly.